Two things to know before we start
The purpose of this page is to explain the process Toolless uses to manufacture a custom plastic enclosure. To do that, we go through the process as if we were making an enclosure to hold a Raspberry Pi 4, something a lot of our customers contact us about.
First, our process does not involve injection molding. All our enclosures start as flat pieces of plastic. A sheet measures 4 by 6 feet, in thicknesses from 2 mm to half an inch. The ABS used in this case has a smooth side and a textured (horse-cell) side. We want the textured side on the outside of the enclosure because the smooth side is extremely susceptible to scratches. For this Pi enclosure we used 3 mm black ABS.
Second, we do not stock enclosures. If you order 50 enclosures, we make the 50. None are waiting on a shelf for someone to order them, and even customers who have been with us for 25 years do not have theirs on a shelf. A change or modification can come at any time, and suddenly that enclosure is out of date. Every customer gets enclosures manufactured as they request more.
Which Raspberry Pi design is it based on?
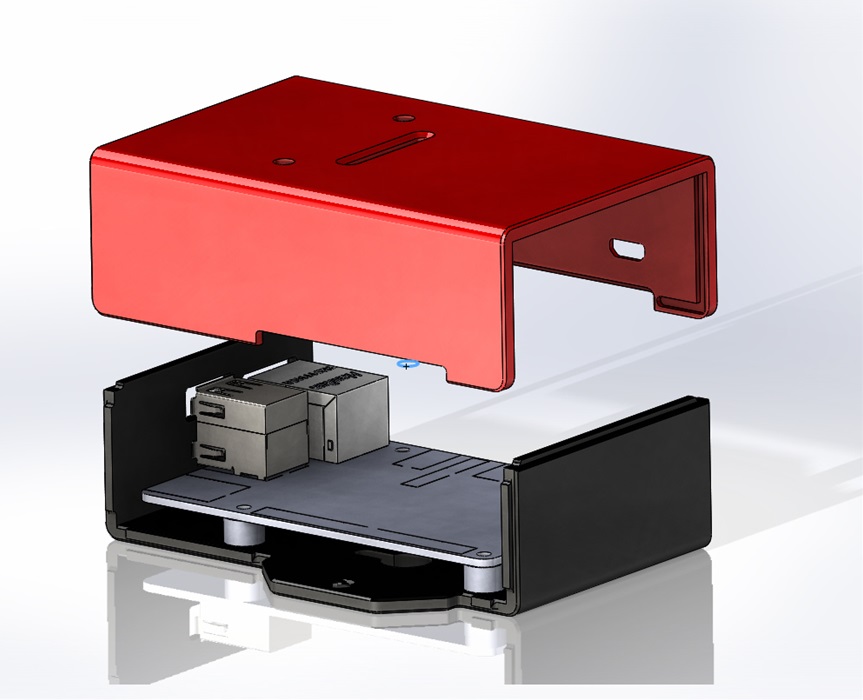
The Pi enclosure made here uses a design we call an EB200 (EB stands for Easy Box). We also refer to it as a “C” box because it ends up as two C-shaped parts that snap together with a tongue-and-groove technique. The process includes seven steps: design, milling or CNC (Computer Numerical Control), saw, printing, bending, assembly and shipping. Each is described below, followed by the options that are possible.
Design details and constraints
Once the sales department has worked out the financial details, the first step is CAD. A CAD designer assigned to your project contacts you and works out the details of your custom plastic enclosure. It is possible to buy an enclosure to house a Pi board, but with Toolless your enclosure is custom made to expose or conceal the components you choose, which opens up a wide range of options to make sure the enclosure has every feature you require.
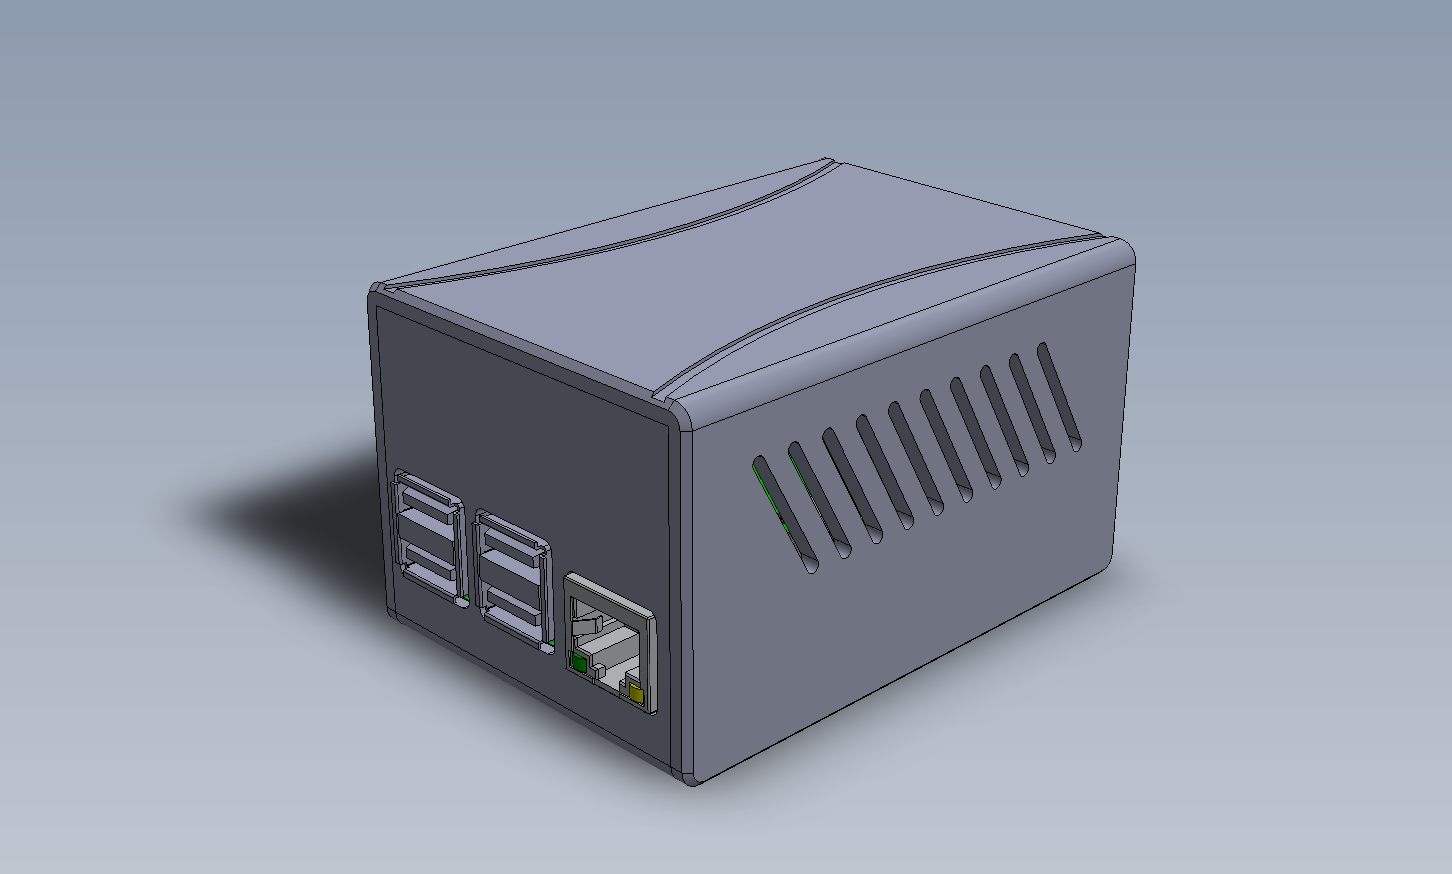
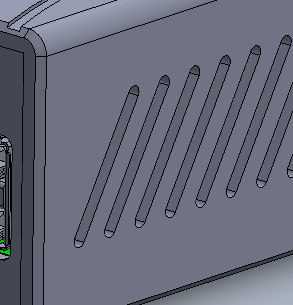
In this example, the customer wanted room for a fan, vents to improve airflow, and access to all the components on the Raspberry Pi 4. The CAD designer’s goals are to provide a functional enclosure, one you are pleased with aesthetically, and one that can be manufactured repeatably: can we repeat the manufacturing process to produce quality enclosures in a time frame acceptable to the customer?
The CAD designer provides a 3D model or 2D drawings to finalize the design. Once the customer approves it, the designer uses the model to write the CNC program and develop a shop traveler.
How we manufacture the custom plastic enclosure
The shop traveler is the manufacturing plan the shop uses to make the enclosure. It gives direction on the material to use, dimensional requirements, the CNC milling order, which bits to use, and special requirements for the saw operator, printer, bend operator, assembly and shipping. With the traveler printed, the job goes to the CNC operator for step 2.
CNC milling
The CNC operator selects a sheet of plastic in the required color and thickness and places it on one of our seven CNC machines. As much milling as possible happens on the smooth side of the plastic, which keeps the textured side, the side the customer sees, as crisp and clean as possible.
Say the first part the operator mills is the inside “C”, the bottom of the enclosure. It is programmed as a flat part with the openings for the USB ports and Ethernet on one side, and the opening for the SD card and two holes to see the LEDs on the other.
The inside dimension of this enclosure is 57 mm wide, 83 mm long and 47 mm high. Flat, the inside part is a rectangle measuring 183 by 59 mm. The 183 is the inside height times two, plus an additional 1 mm on each end for the feeders, plus 6 mm more (3 mm for each of two bend cuts). The 59 is the inside width plus 1 mm feeders on each side. Confusing on its own, but our CAD designers, with the help of SolidWorks, are quite capable of creating the programming needed to mill the correct parts.
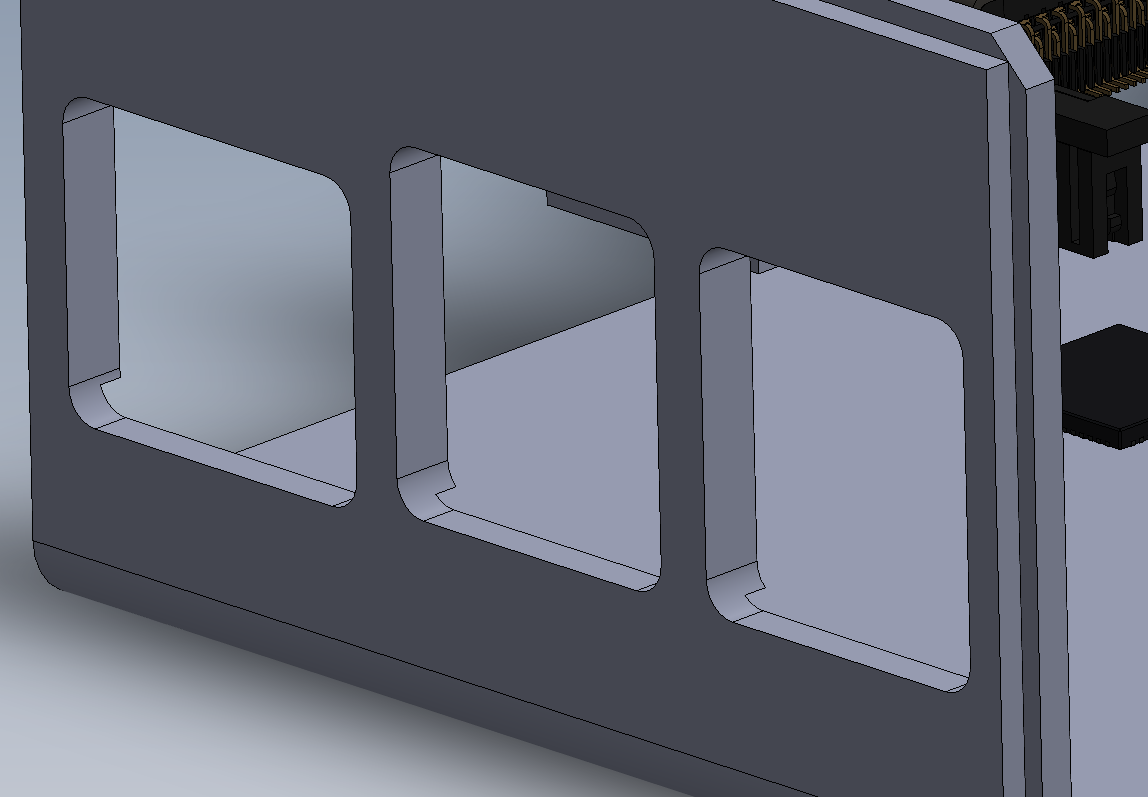
The CNC process
The operator mills one part and evaluates the outcome. A general observation checks that every feature on the traveler matches the milled part, then a dimensional check covers length and width, hole diameters, the depth of any recesses, and any other dimension the CAD designer considers critical. If an error is detected, the CNC operator consults the CAD designer to resolve it. Once everything checks out, the operator mills the required number of parts.
After the inside “C”, the outside “C” (the top of the box) starts milling. In this case it has cutouts for the USB-C, the micro HDMI ports and the audio jack, and a slot near the outside perimeter that accepts the feeder holding the enclosure together. The outside C is also milled on the smooth side. The CNC has been programmed to make a frame that accepts the milled part and lets the operator mill the other side, which creates the recess for the HDMI ports and the USB-C and adds a couple of decorative grooves across the top. When milling is complete, both parts go in a labeled bin and move to the next operation.
Quantity
The number of parts milled is always more than the order requires. If you order 25 enclosures, the CNC operator looks at the number of operations that follow milling and increases the count to compensate for tests and machine setup in those later operations. In this example, we would expect the operator to make 6 extra parts.
Saw
Step 3 is the saw, which makes two kinds of cuts: feeders and bend cuts. We have three large table saws with the blades mounted from below. The saw operator takes a scrap piece of plastic of the same thickness as the part, refers to the dimensions on the traveler, adjusts the saw and cuts the scrap. After the necessary adjustments, the first real part is cut. This is where the extra parts are sometimes needed: if a cut is out of tolerance, there is one less part to use.
The first blade used is normally a 90-degree blade that cuts the “bend groove”. The width of the bend groove is normally the same as the thickness of the material, so in this case 3 mm. The other blade is a flat blade that cuts the feeder. Again the operator makes several test cuts on scrap before cutting the milled parts, then tests the fit of the two pieces and makes several dimensional checks to make sure the parts are within tolerance.
The traveler sets the order of operations. After the saw, a part typically goes to printing if needed, or to bending. Occasionally a part goes straight to assembly or shipping after the saw; it depends on the enclosure and its needs.
Printing
Step 4 is printing. We have three printers for printing on parts. Sometimes a customer wants a logo; other times they want labels (on/off, HDMI, input, output and so on) next to the cutouts and slots. We use UV solvent ink and can print multiple parts at a time, depending on the size of the part. The printed parts then move on to the next operation, typically bending.
Bending
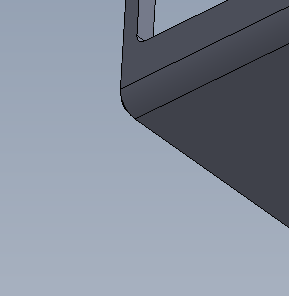
This is where the parts take the “C” shape of the custom plastic enclosure. We have several bending machines that work on the same technique. The operator sets up the bending table to match the size of the part. The tables heat the area along the bend cuts while adding pressure to the part, and once the pressure exceeds the plastic’s ability to remain flat, the part bends to a 90-degree angle. Each of the two parts for the Pi box needs two bend operations. The bending operator makes dimensional checks and a test fit after the parts take shape, then the two “C” parts move to the assembly area.
Assembly
Assembly is an optional operation that depends on the customer’s needs. This is where we install any accessories the enclosure requires. Each type of plastic has its own bonding procedure to secure accessories properly. Accessories we can add include standoffs, inserts, light pipes, screws, acrylic windows, tabs and more. When a traveler first arrives in assembly, the assembly lead builds a setup box: the complete enclosure with every operation and accessory. The CAD designers review the setup box for approval and dimension checks, and once it is approved the remaining parts go through assembly. Parts that require bonding or glue stay in the assembly area until they cure before moving to shipping.
Shipping
Shipping has two responsibilities. It is the final operation that makes sure the custom plastic enclosure is a quality product: the parts are cleaned and inspected for fit and form, and the traveler is checked for any specific instructions on testing or quality checks. The final stage is packing the enclosures to prevent damage in transit, then addressing and shipping them by the best method.
The final product, and the options
The enclosure in this example secures the board with internal slots and the inside surface of the enclosure. If you did not want access to the SD card, we would move the board away from that surface and use circular standoffs (also called bosses or spacers). A soldering iron melts brass threaded inserts into each standoff, and circular recesses milled into the bottom align the standoffs for gluing.
The list of options is almost endless: the color, thickness and texture of the plastic, which components are exposed, reversing the “C”, adding flanges for mounting, or securing the enclosure with tabs. It all starts with the CAD designer and a conversation about how you want your enclosure to look.
Ready for a case of your own? See the custom Raspberry Pi cases we have built, start from the C Box this one is based on, or read about the full manufacturing process.